As a supplier of Servo Hybrid Vertical Injection Moulding Machines, I’ve witnessed firsthand how these remarkable pieces of equipment revolutionize the plastic manufacturing industry. One of the most critical processes in this field is the melting of plastics within the machine. In this blog, I’ll delve into the science and mechanics behind how the melting process of plastics in a servo hybrid vertical injection moulding machine works. Servo Hybrid Vertical Injection Moulding Machine

The Basics of Servo Hybrid Vertical Injection Moulding Machines
Before we explore the melting process, let’s briefly understand the servo hybrid vertical injection moulding machine. This type of machine combines the advantages of servo – motor technology and hydraulic systems. The vertical design offers unique benefits such as easy handling of inserts, reduced floor space requirements, and better access for operators. The servo – motor provides high precision and energy efficiency, while the hydraulic system offers the necessary power for the injection process.
Starting with Plastic Pellets
The journey of plastic melting begins with plastic pellets, which are small, uniform granules of plastic resin. These pellets are the raw material for the injection moulding process. Different types of plastics, such as polyethylene (PE), polypropylene (PP), polystyrene (PS), and polycarbonate (PC), have different melting points and characteristics, which will influence the melting process.
Feeding the Plastic Pellets
The plastic pellets are first loaded into the hopper of the injection moulding machine. The hopper is designed to hold a sufficient quantity of pellets to ensure a continuous supply during the manufacturing process. From the hopper, the pellets are fed into the heating barrel by a screw mechanism. This screw rotates, gradually moving the pellets forward towards the heated zone of the barrel.
Heating the Plastic in the Barrel
The heating barrel is a crucial component where the actual melting of the plastic takes place. It is equipped with multiple heating bands along its length. These heating bands are electrically powered and can be individually controlled to maintain a specific temperature profile.
The temperature profile along the barrel is carefully designed to gradually increase the temperature of the plastic. At the beginning of the barrel, where the plastic pellets enter, the temperature is set relatively low. This initial stage is important as it helps to pre – heat and soften the pellets without causing them to melt too quickly. As the plastic moves further along the barrel, the temperature increases, reaching the melting point of the specific plastic resin being used.
For example, polyethylene has a melting point range of around 105 – 137°C (221 – 279°F), while polycarbonate has a much higher melting point, typically around 220 – 260°C (428 – 500°F). The heating bands are adjusted accordingly to ensure that the plastic reaches its melting point at the appropriate location in the barrel.
The Role of the Screw
The screw inside the heating barrel plays a vital role in the melting process. As it rotates, it not only moves the plastic pellets forward but also performs two other important functions: mixing and shearing.
Mixing
The screw is designed with flighted segments that create a turbulent flow of the plastic pellets. This turbulence helps to mix the plastic, ensuring that any additives or colorants are evenly distributed throughout the material. A uniform mixing is essential for producing high – quality plastic products with consistent properties.
Shearing
Shearing is another critical aspect of the melting process. As the screw rotates, it applies a shearing force to the plastic. The shearing effect generates friction within the plastic, which in turn produces heat. This additional heat, combined with the heat from the heating bands, helps to accelerate the melting process. The shear rate can be controlled by adjusting the rotational speed of the screw. A higher rotational speed results in a higher shear rate, which can lead to faster melting but also needs to be carefully balanced to avoid over – heating and degradation of the plastic.
Measuring and Controlling the Melt Temperature
Accurate control of the melt temperature is essential for a successful injection moulding process. Temperature sensors are placed at various points along the heating barrel to monitor the temperature of the plastic. These sensors send real – time data to the machine’s control system.
The control system, which is often based on advanced programmable logic controllers (PLCs), compares the actual temperature with the set – point temperature. If there is a deviation, the control system adjusts the power supplied to the heating bands or the rotational speed of the screw to bring the temperature back to the desired level.
Plastic Melt Preparation and Injection
Once the plastic has completely melted in the barrel, it is ready for injection into the mould. The screw stops rotating and acts as a plunger, pushing the molten plastic towards the nozzle at the end of the barrel. The molten plastic is forced through the nozzle and into the mould cavity under high pressure.
The pressure required for injection can vary depending on the type of plastic, the design of the mould, and the size and complexity of the product. The servo – motor and hydraulic system work together to provide the precise amount of pressure needed for a successful injection.
Post – Melt Considerations
After the plastic has been injected into the mould, it needs to cool and solidify to take the shape of the mould cavity. During this cooling stage, the properties of the plastic, such as its shrinkage rate, can affect the final dimensions and quality of the product. Therefore, the cooling system of the injection moulding machine is also an important part of the overall process.
Why Our Servo Hybrid Vertical Injection Moulding Machines Excel in the Melting Process
Our machines are designed with state – of – the – art technology to ensure a smooth and efficient melting process. The temperature control system is highly accurate, allowing for precise adjustment of the heating profile based on the specific requirements of different plastics. The screw design is optimized for maximum mixing and shearing, ensuring uniform melting and distribution of additives.
The servo – motor technology provides excellent energy efficiency and high – speed response, which is crucial for maintaining the right balance of heat generation during the melting process. The hydraulic system, on the other hand, offers the power needed for high – pressure injection, ensuring that the molten plastic fills the mould cavity completely.
Contact Us for Your Plastic Moulding Needs
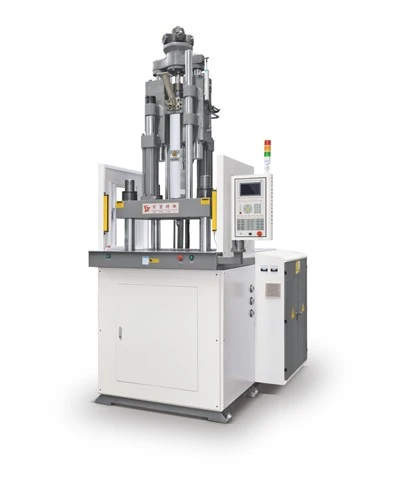
If you are in the market for a reliable servo hybrid vertical injection moulding machine for your plastic manufacturing business, we are here to help. Our machines are engineered to provide the best performance in the melting and injection processes, ensuring high – quality products and cost – effective production.
Slide Table Vertical Injection Moulding Machine We understand that every customer’s requirements are unique, and our team of experts is ready to work with you to find the perfect solution for your specific needs. Whether you are a small – scale operation or a large – scale manufacturer, we can provide the right machine and support to help you achieve your production goals. So, don’t hesitate to reach out to us to start a discussion about purchasing the ideal servo hybrid vertical injection moulding machine for your business.
References
- Osswald, T. A., & Menges, G. (2003). Materials science of polymers for engineers. Hanser Gardner Publications.
- Rosato, D. V. (2000). Injection molding handbook. Kluwer Academic Publishers.
Guangdong Baizan Intelligent Equipment Co., Ltd.
We are one of the most professional servo hydraulic vertical injection moulding machine manufacturers and suppliers in China. We warmly welcome you to buy customized servo hydraulic vertical injection moulding machine at competitive price from our factory. If you have any enquiry about pricelist and quotation, please feel free to email us.
Address: No.8, Jianye Road, Dahuai Town, Enping City, Jiangmen City, Guangdong
E-mail: wjx@baizanjx.com
WebSite: https://www.baizanplast.com/
